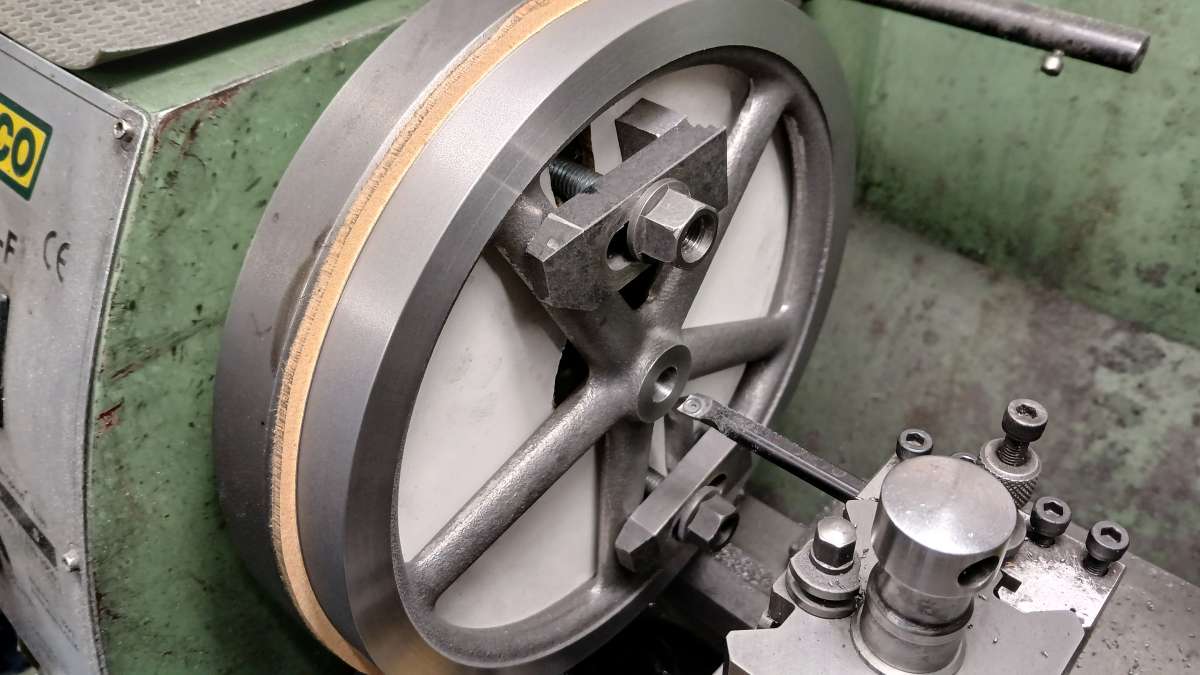
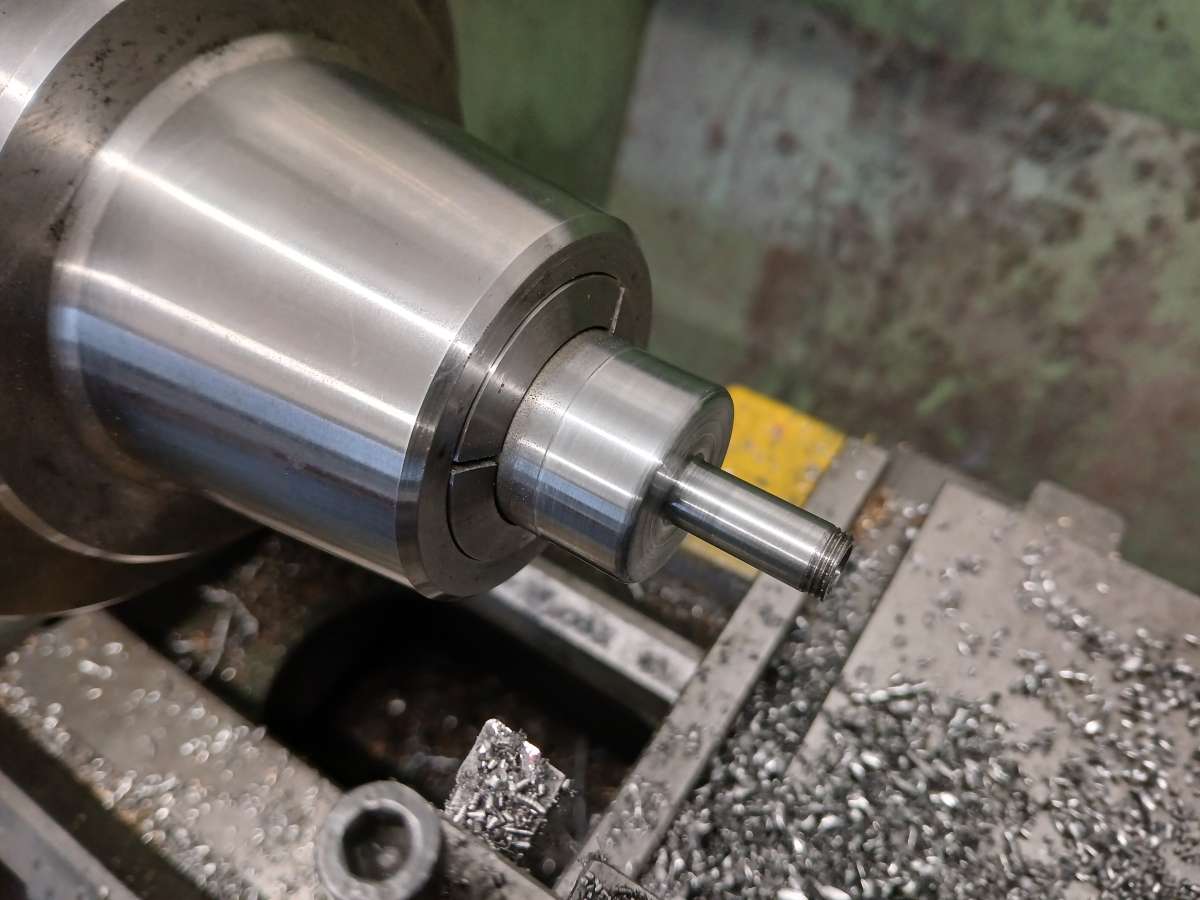
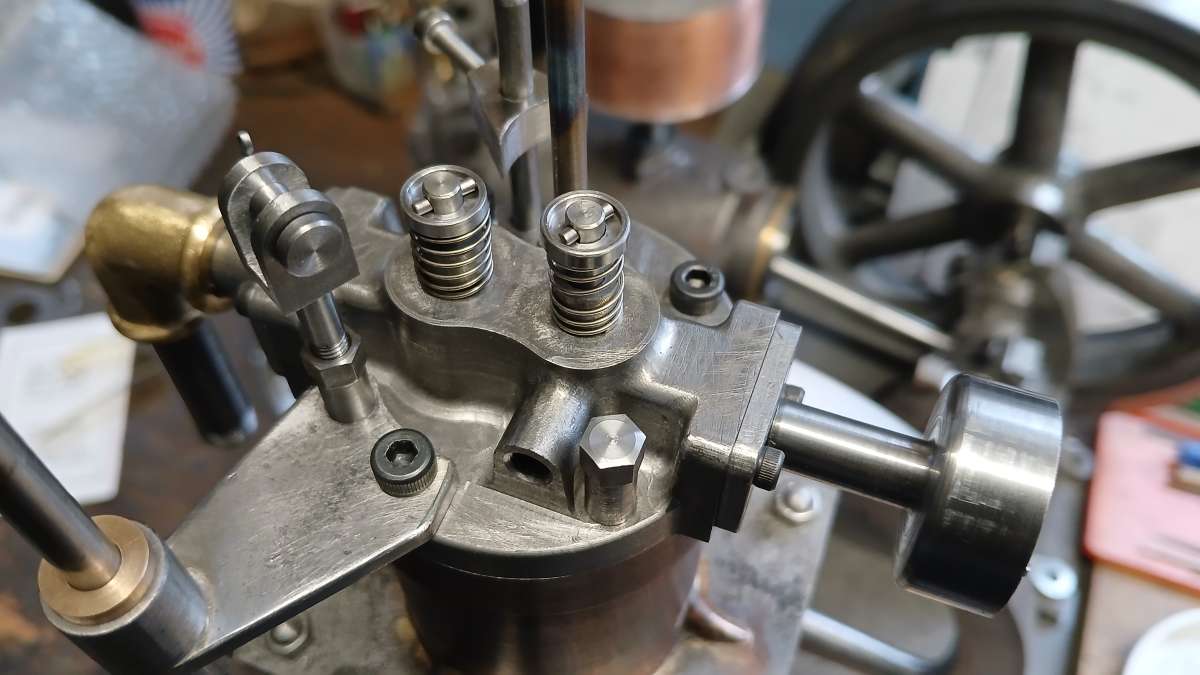
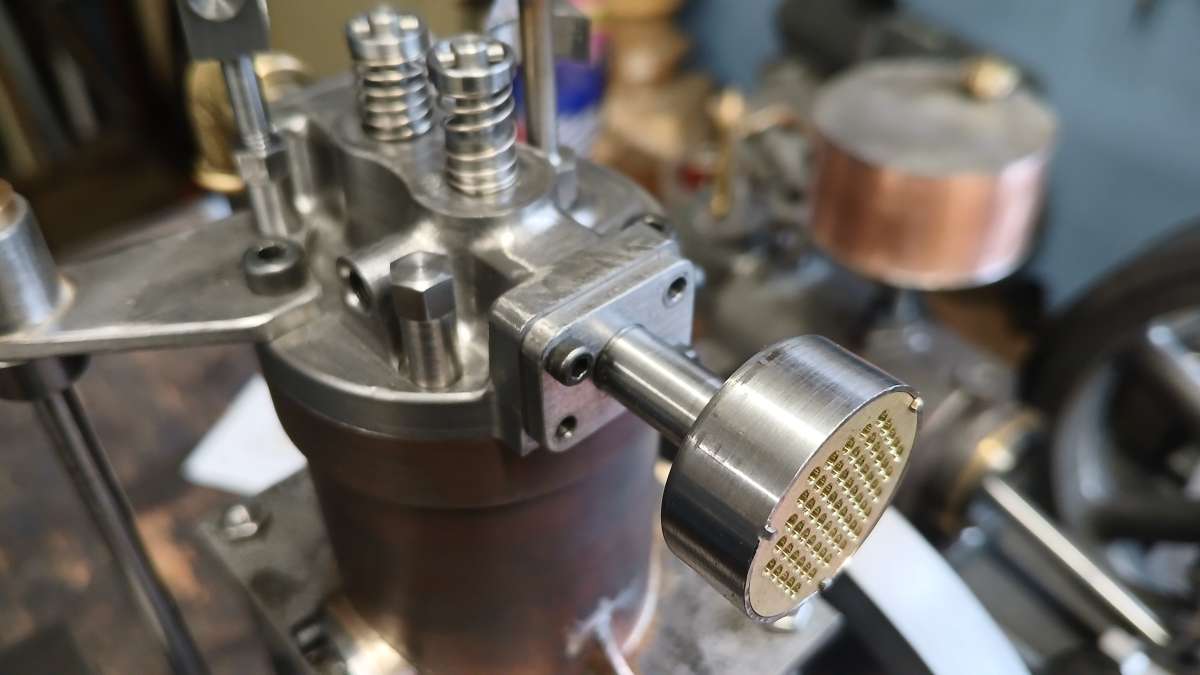
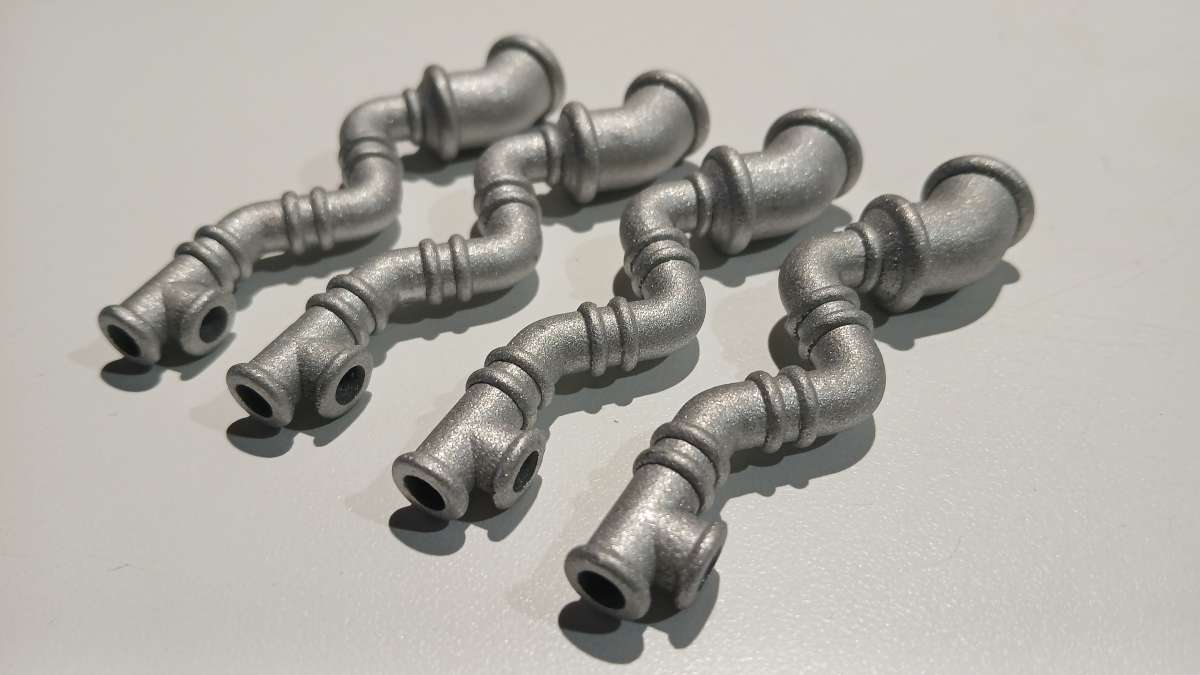
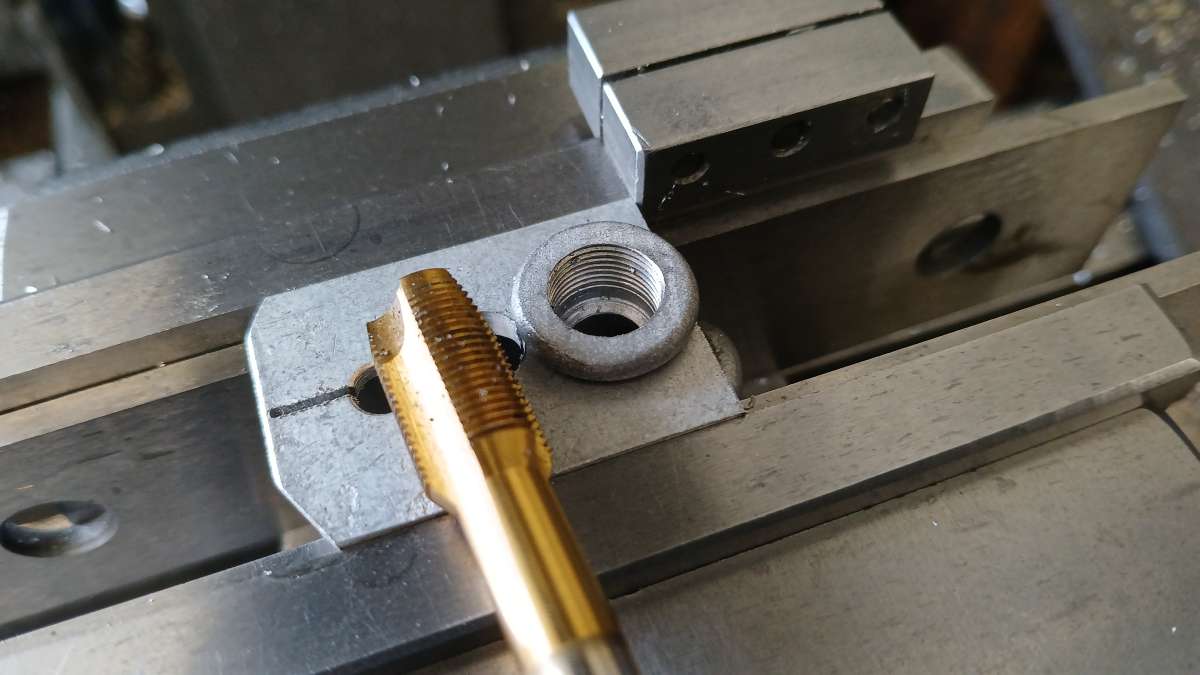
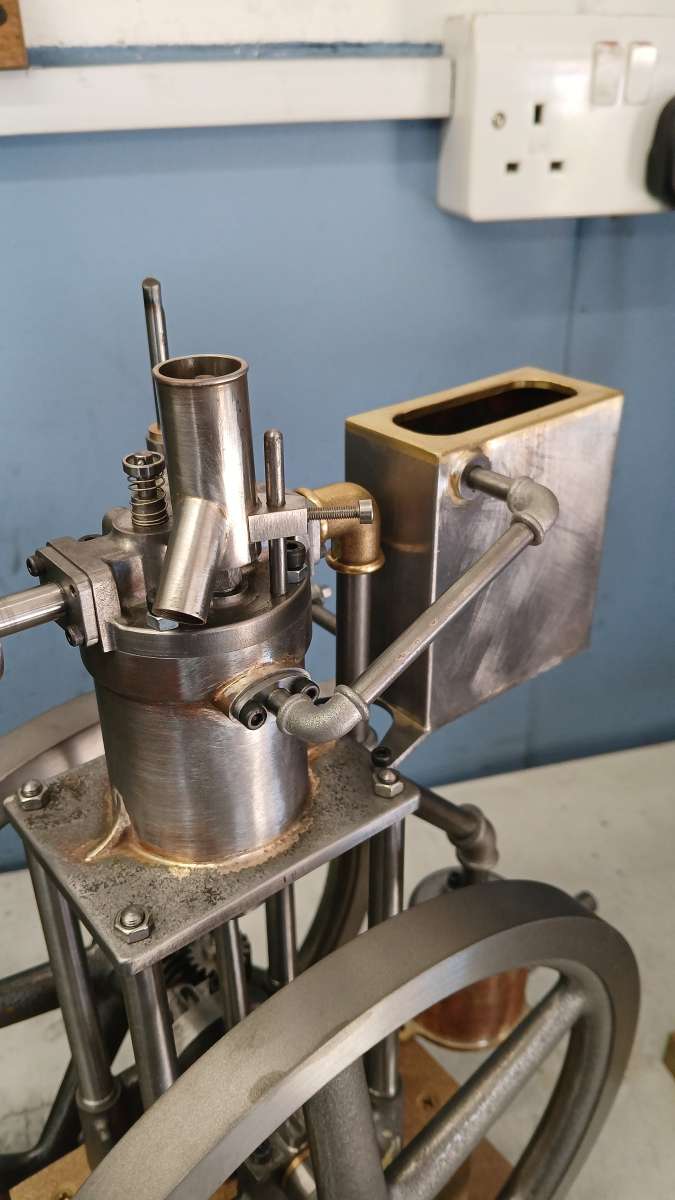
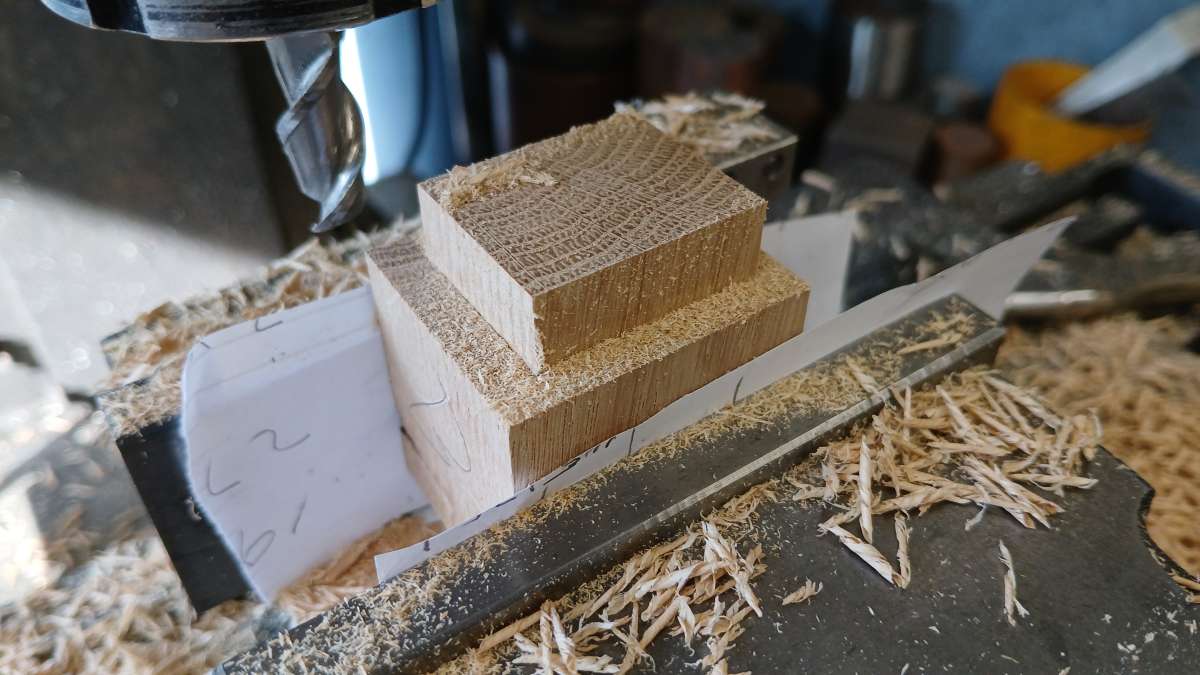
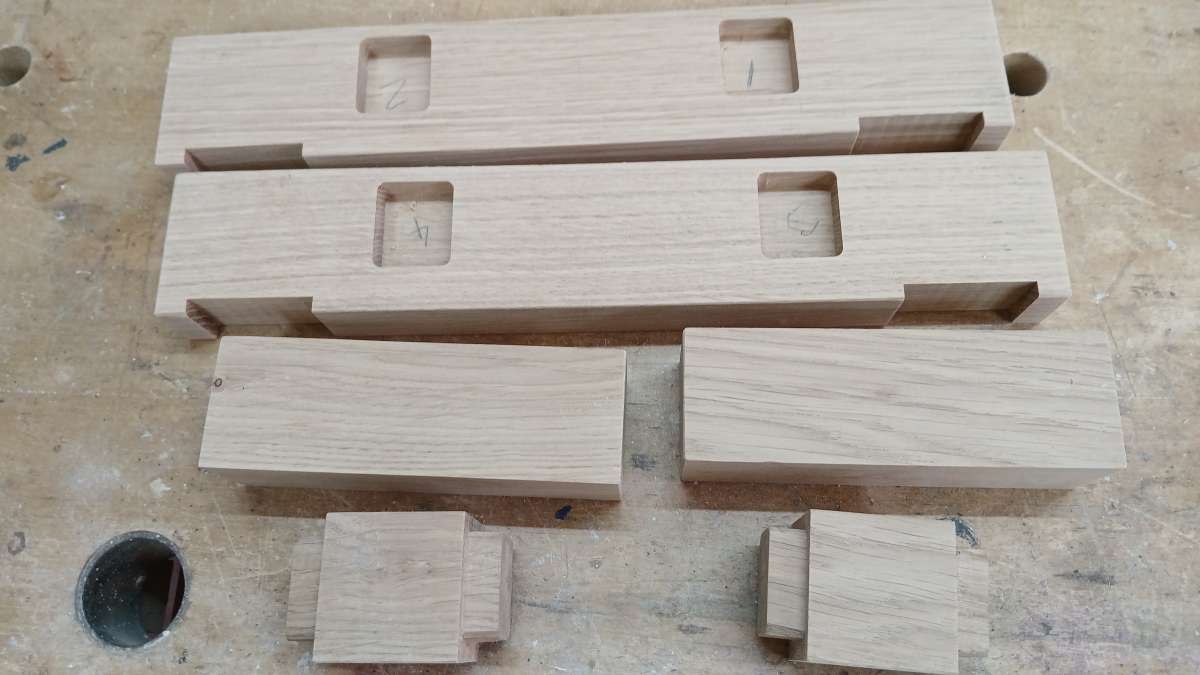
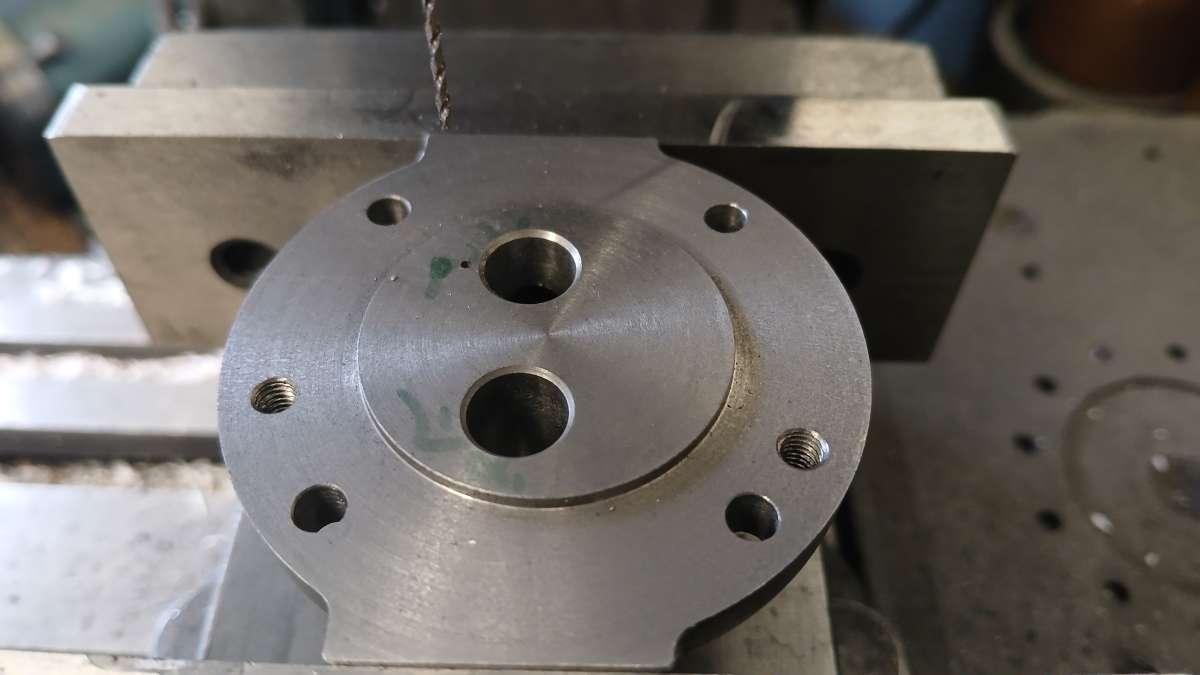
The first job was to machine the underside of the head including a spigot to locate in the cylinder liner. I then moved over to the mill and tapped what will eventually be the clearance holes for the head studs so that I could screw the head to a holding plate to give easy access all round for machining. I also ctr drilled the position of the valves at the same setting.
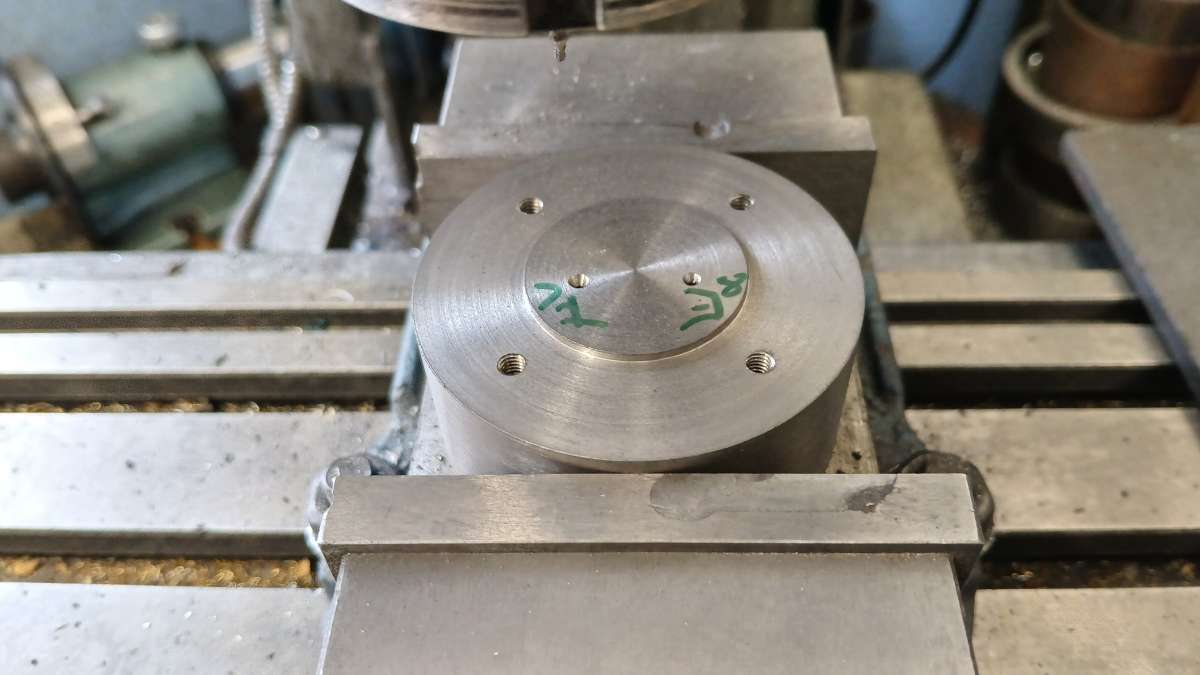
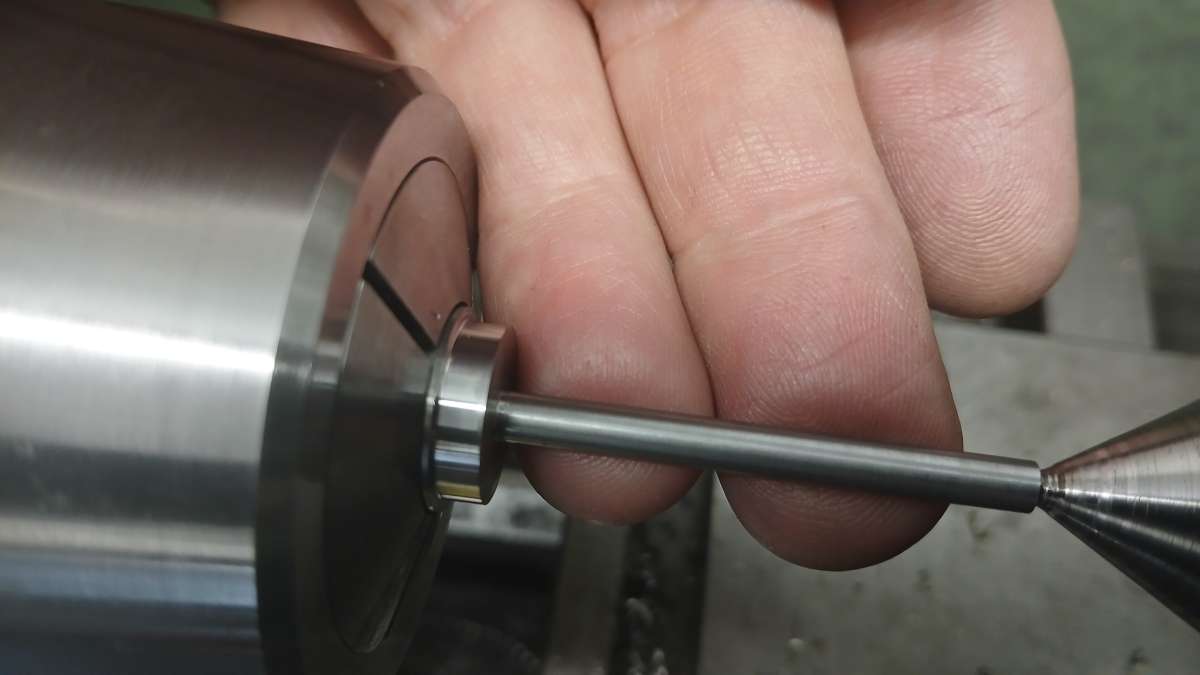
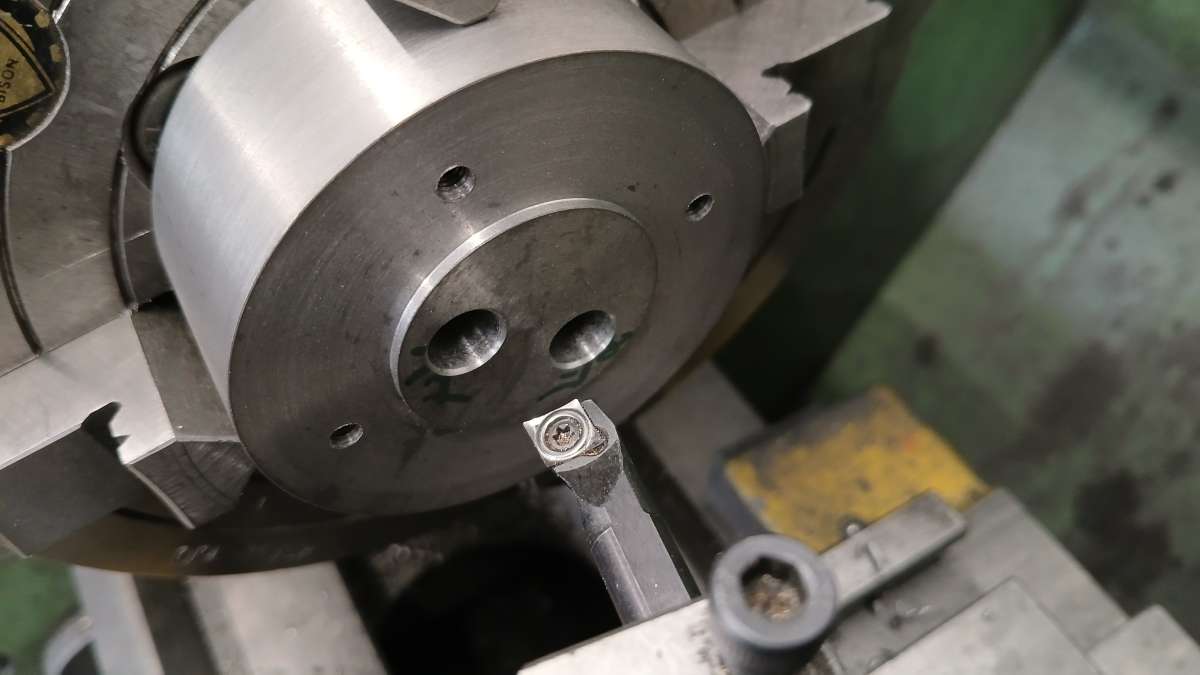
Back on the lathe the valve guide holes were clocked in, drilled and reamed, the cavity behind the valve heads opened up and the seats cut at 45deg using the top slide which keeps everything concentric. I actually only needed to angle the exhaust valve seat but got carried away and did both!
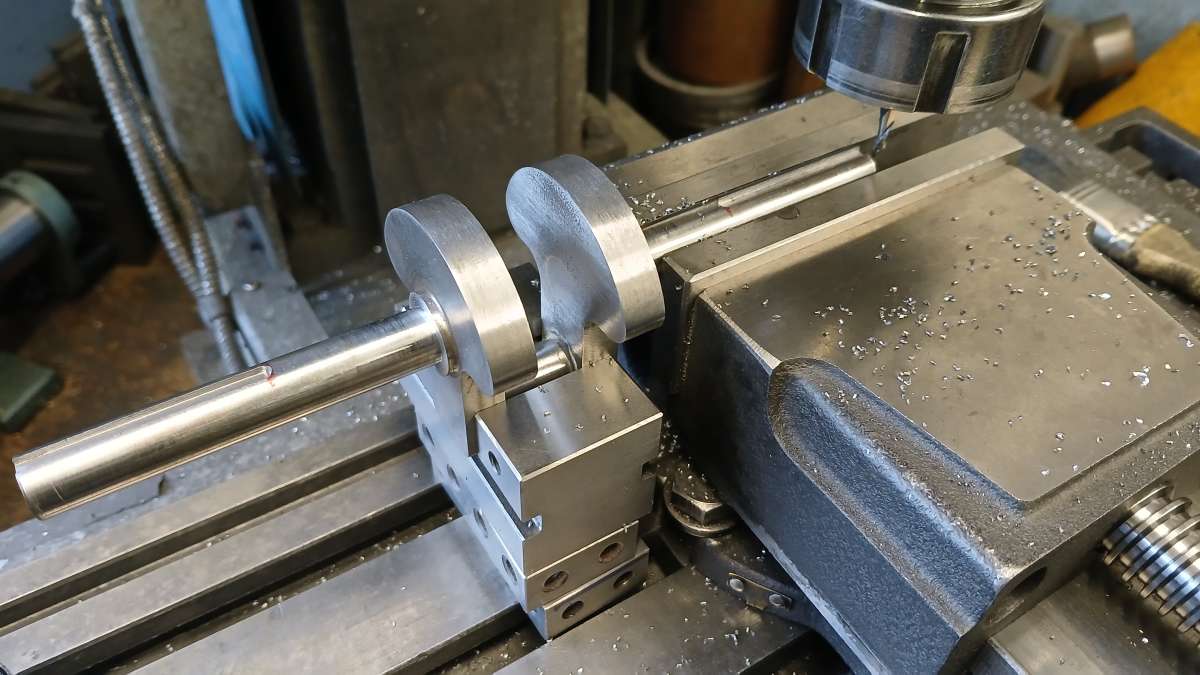
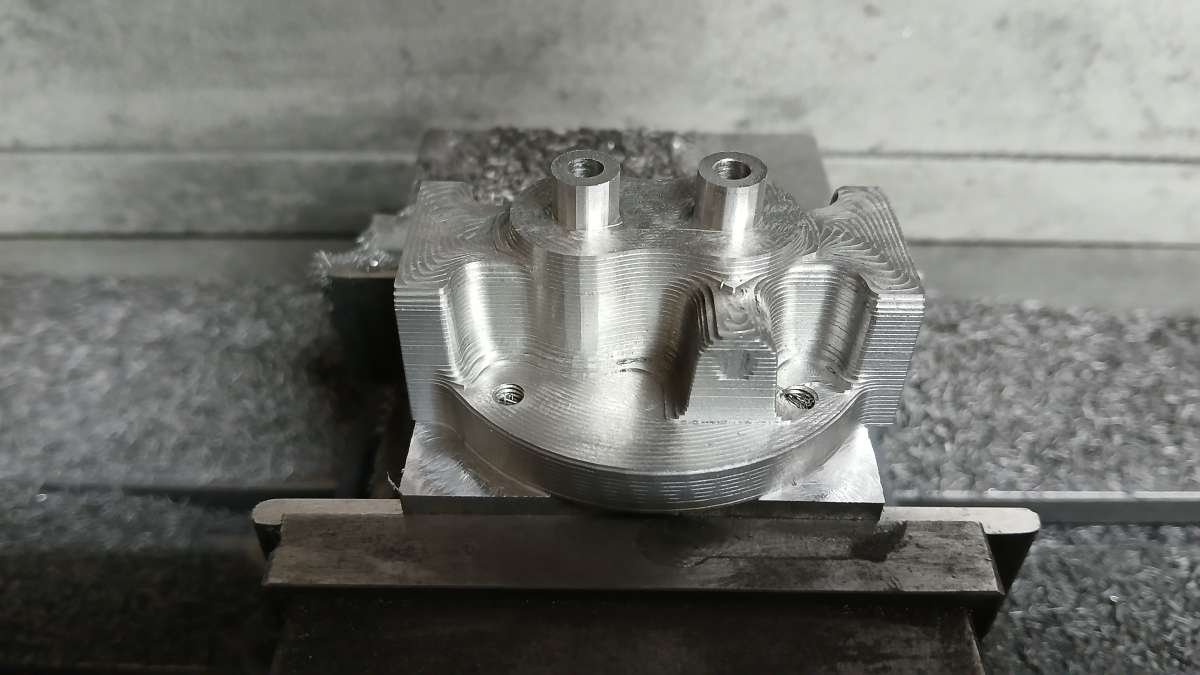
Then onto the CNC, this image shows the contoured effect that the initial adaptive cuts leave.
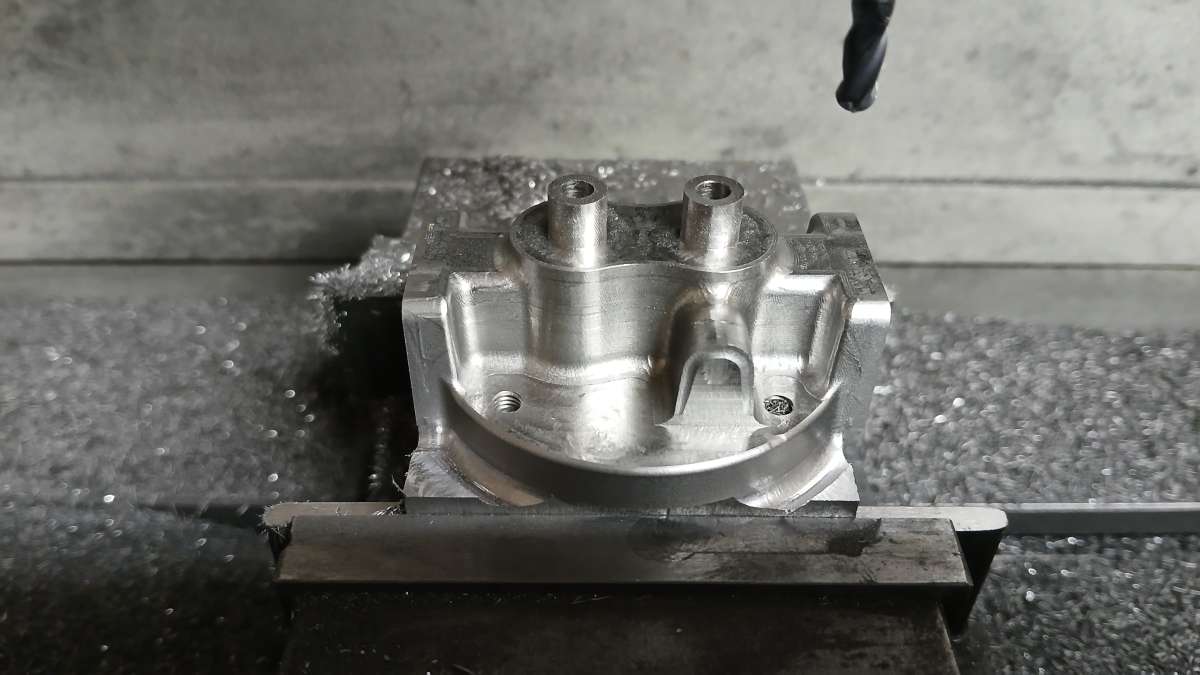
Then various other paths were run to shape the "cast" surfaces with their draft angles and leave the "machined" faces flat and true
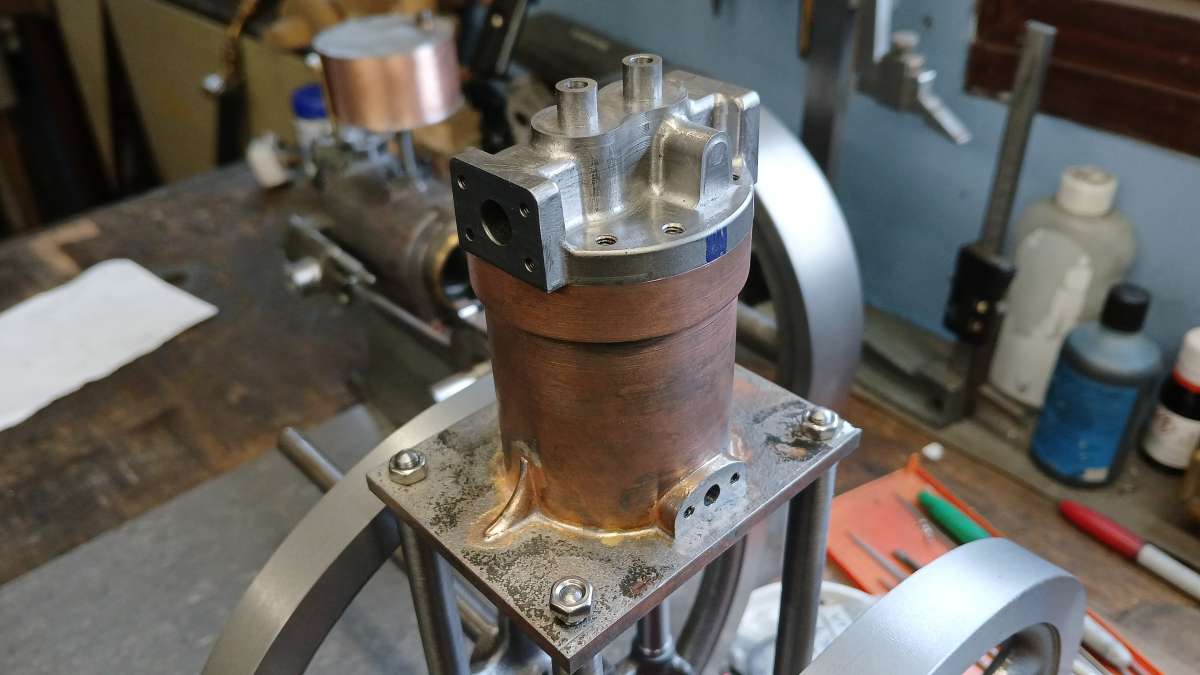
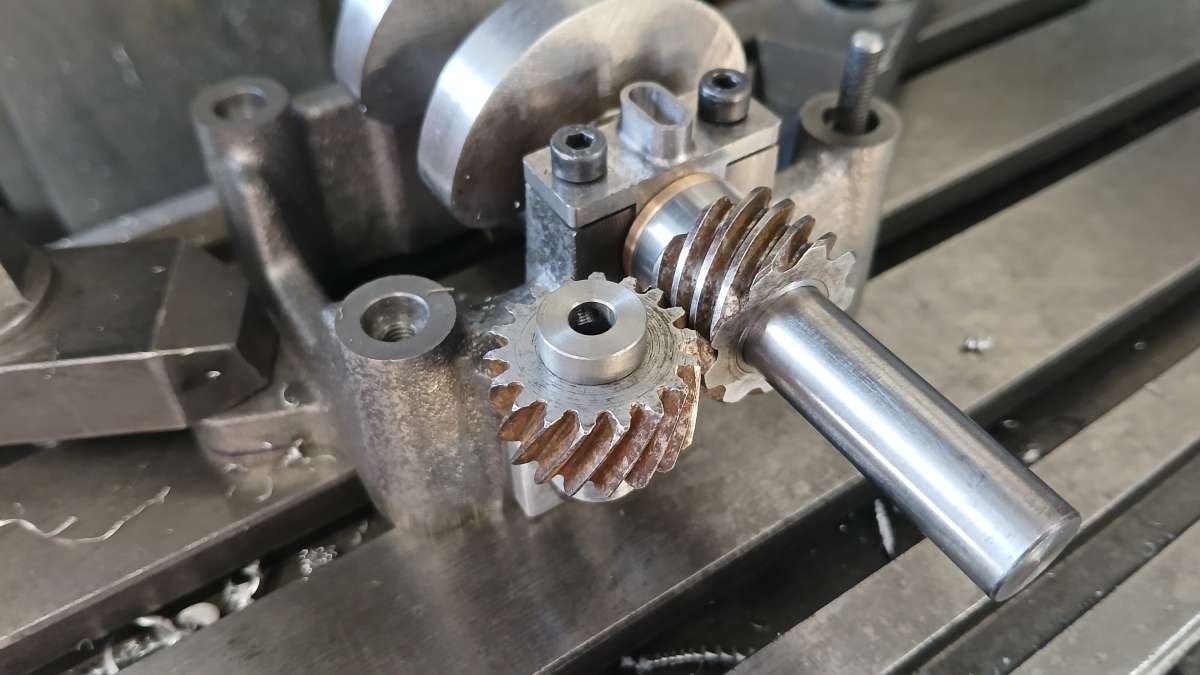
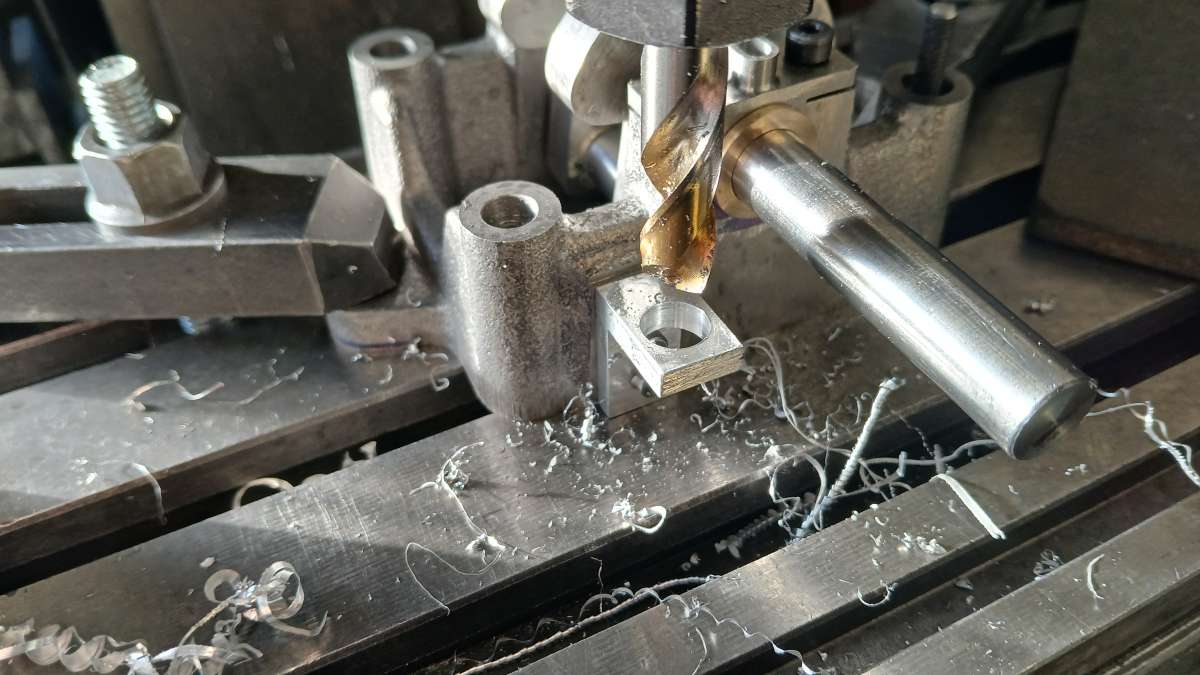
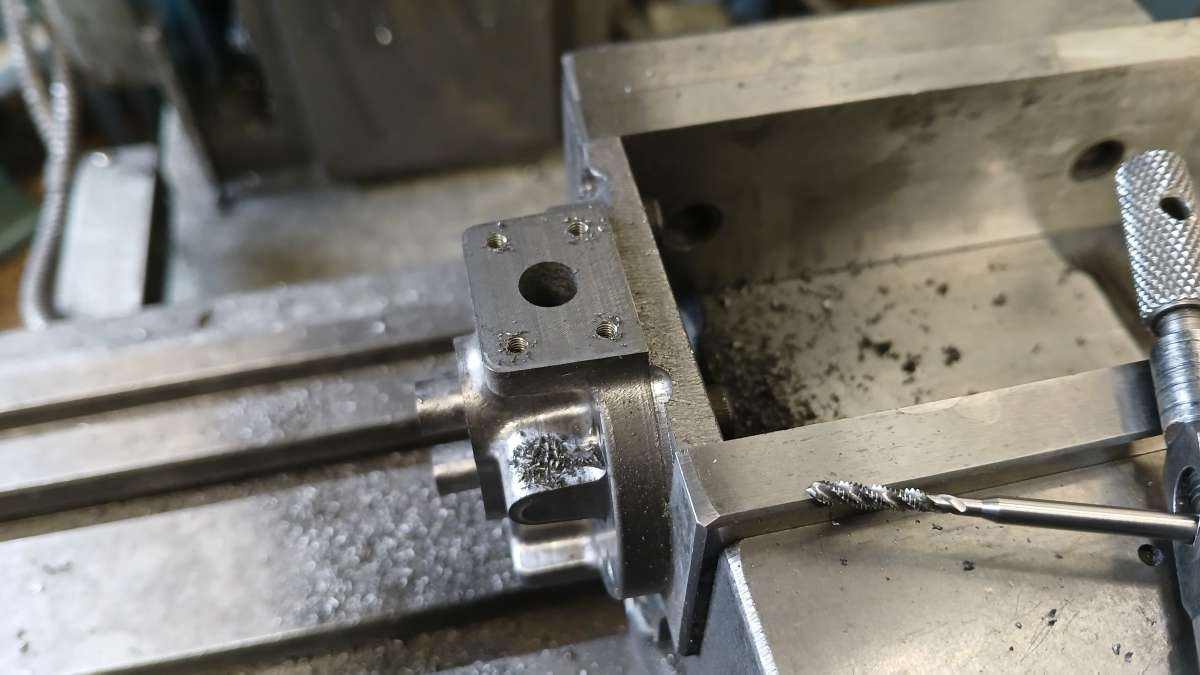
With the head still attached to the holding plate it was easy to hold on the manual mill for the last few operations which were mainly the inlet and exhaust passages and the tapped holes around those for flanges.
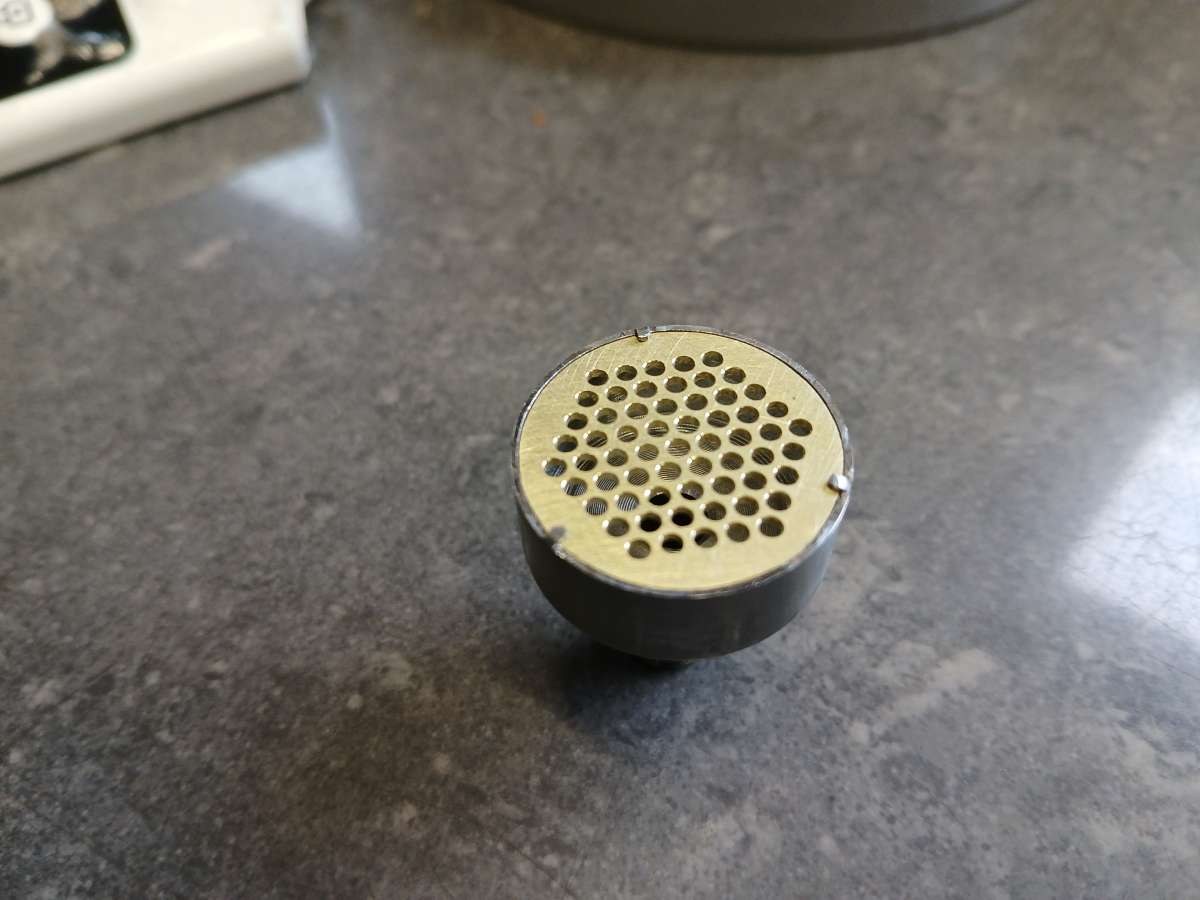
This engine has an atmospheric inlet valve where the vacuum caused by the descending piston opens the valve, this can also be used to act as a demand valve for the Propane gas that will fuel the engine by having the flat valve also cover a small 0.7mm gas passage.
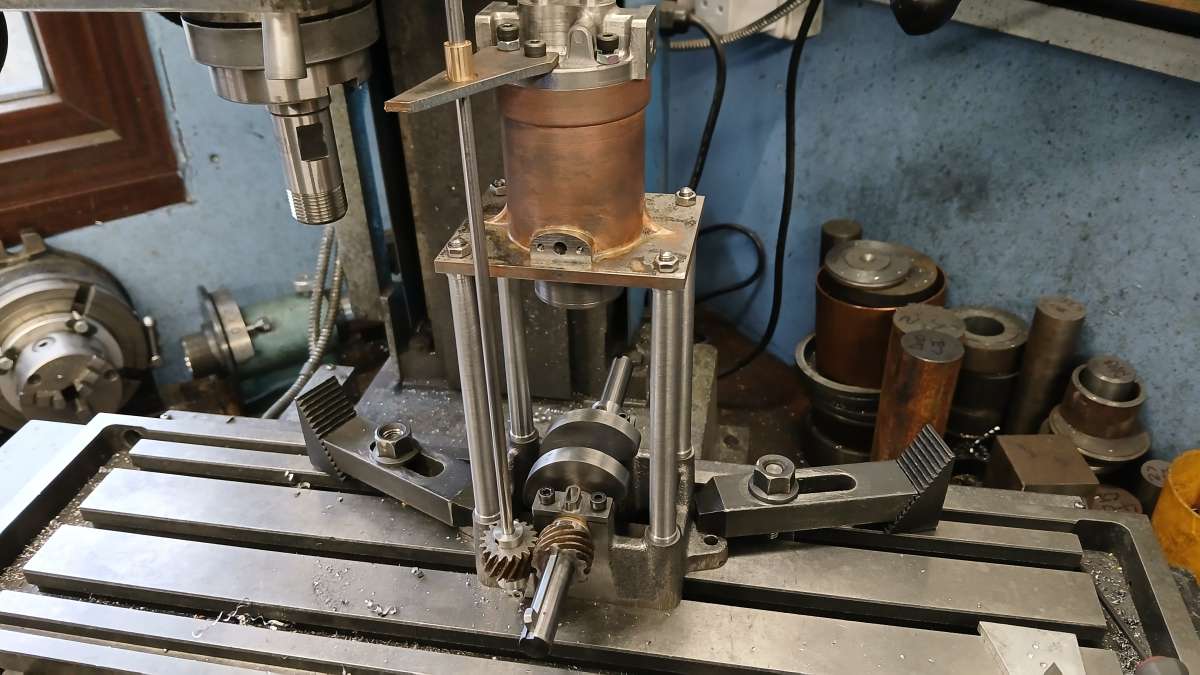
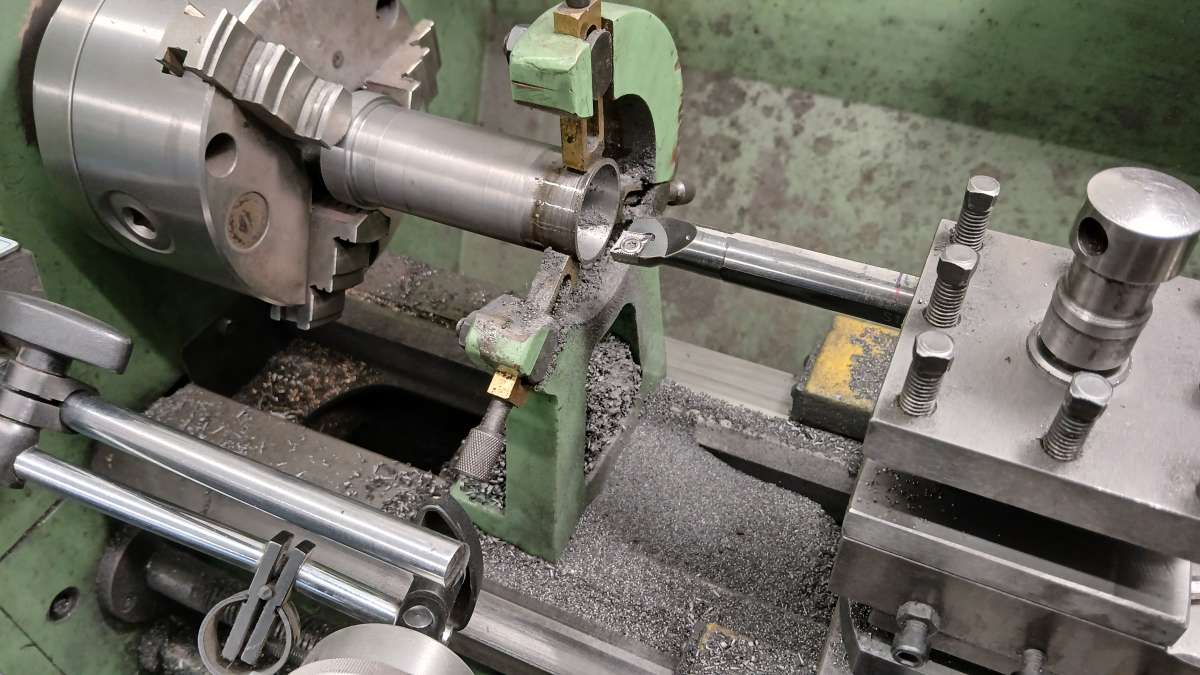
The original would have had a water jacket cast in around the cylinder with the water space being formed by a sand core. For our models it is easier to have a separate liner that as well as forming the cylinder also closes off the waterspace. Here the OD has been machined and a steady is in use while the cast iron bar is bored to size. I leave a bit of solid material at the end so that the chuck will not distort the thin liner, this can be cut off afterwards and the liner faced to length.
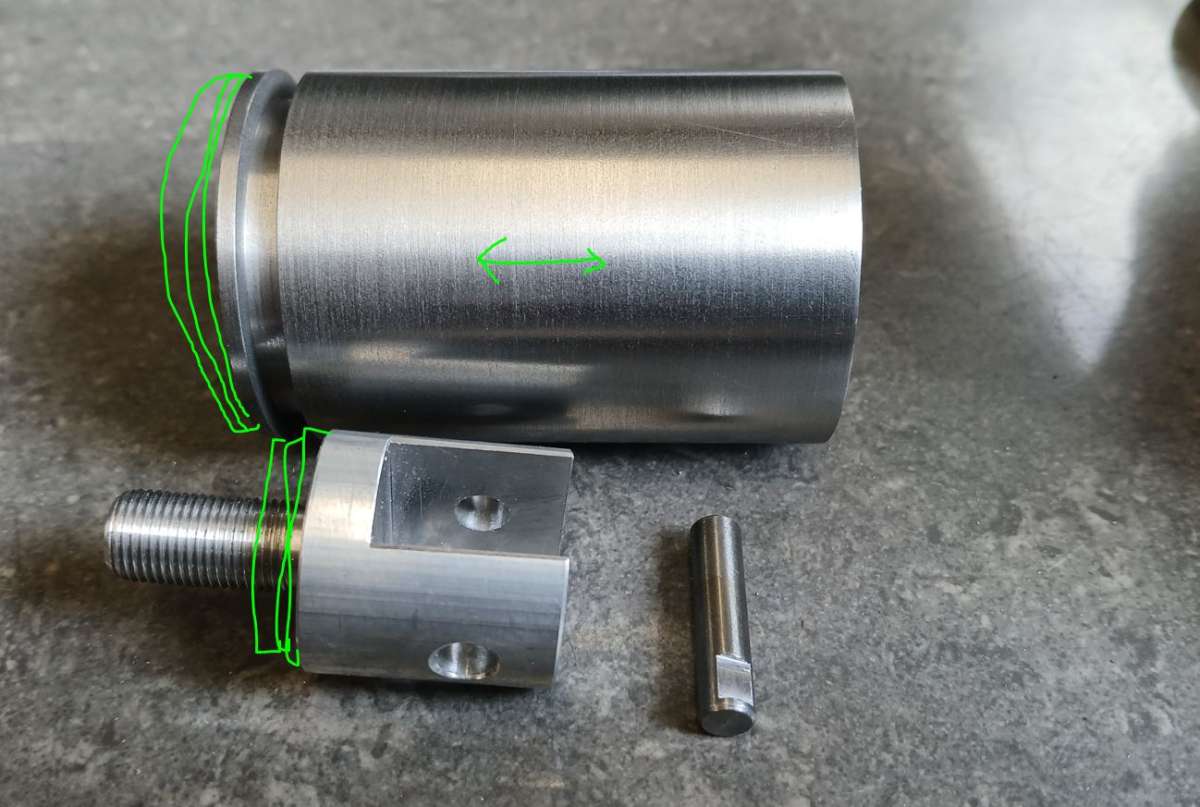
The cylinder does protrude below the bottom of the entablature and as the liner would have been too thin I turned up a sleeve to add the additional thickness. It also allowed me to silver solder on a bush for a drip feed oiler. Liner, Cylinder jacket and sleeve were all a push fit and assembled with 648 Loctite.