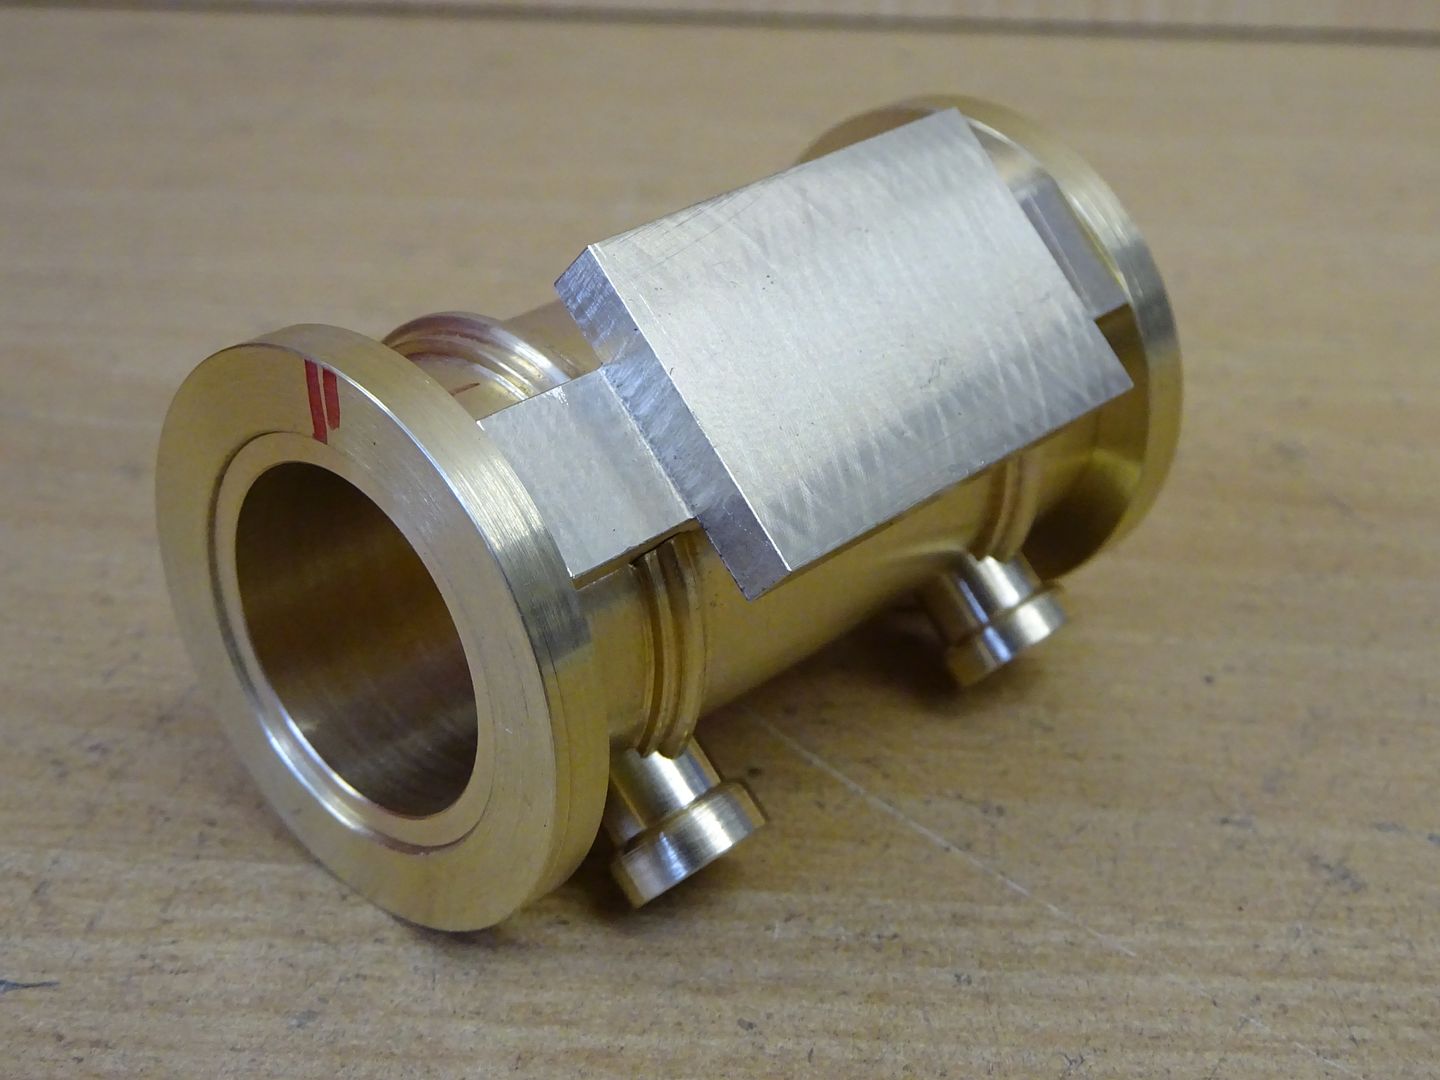
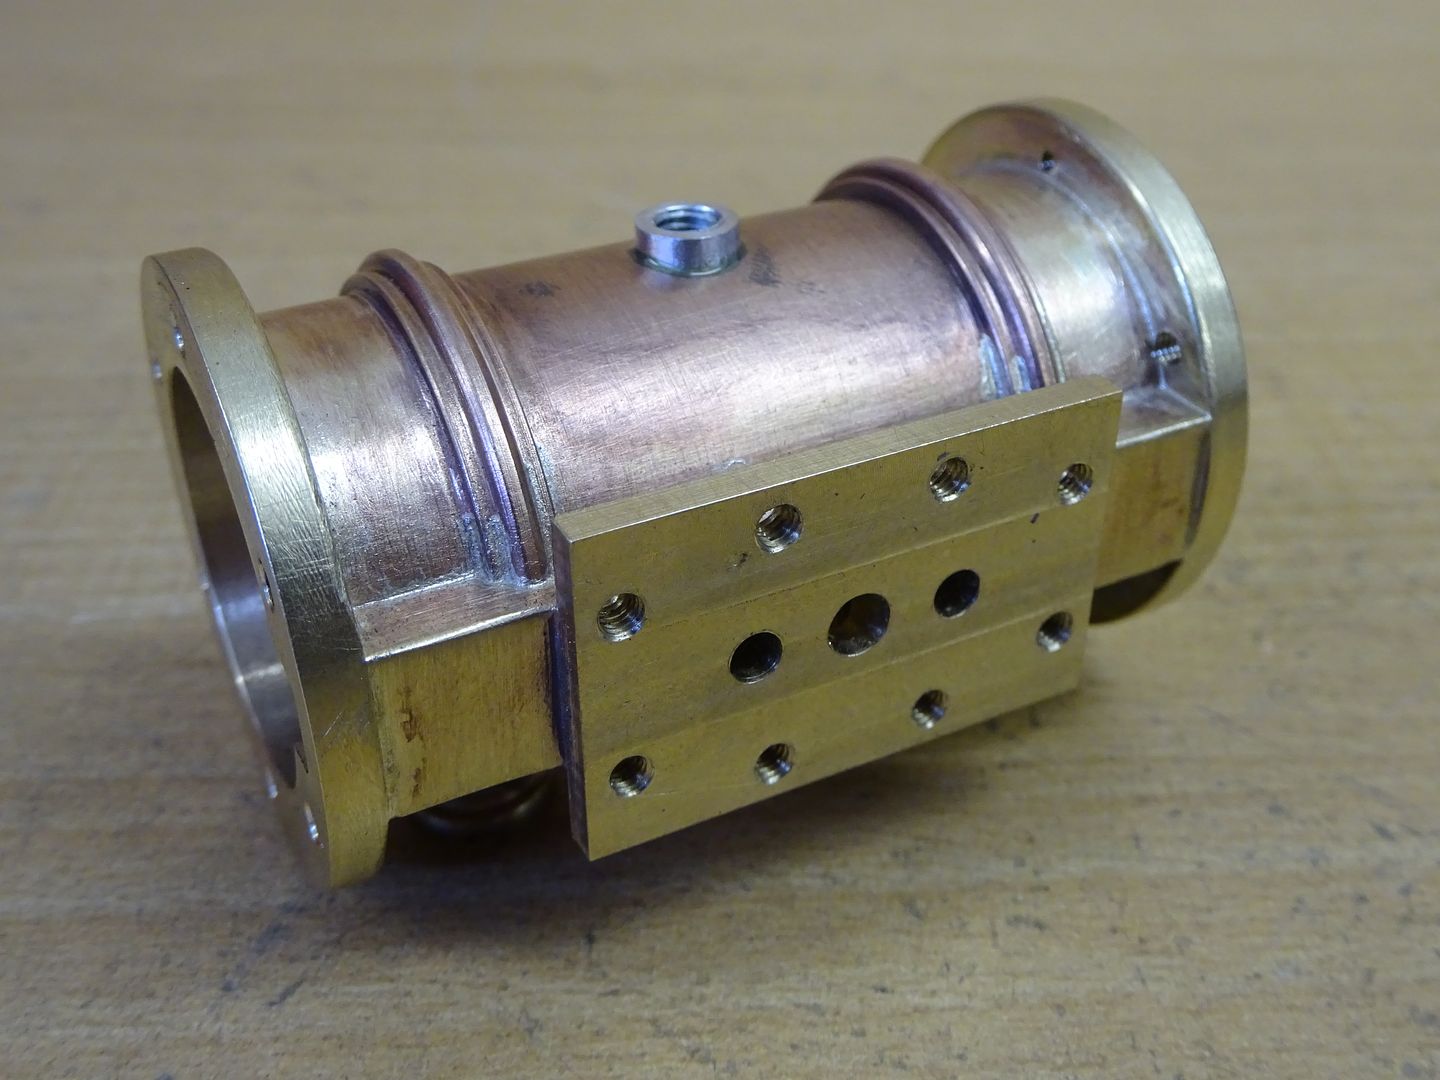
Adventure in astragals on the menu today.
as·tra·gal
noun
ARCHITECTURE: a small semicircular molding around the top or bottom of a column.
Leave it to Jason to know the name for these decorations. Since the Benson engine has 2 of these on the column and 1 on the cylinder, I think it behooves me to know how to turn one before diving in for a fabrication (on casting set they're already on the castings).
The obvious solution is a form tool, and other than a couple of rough grinds I haven't made any. I did buy one for forming the rims on the wheels of my locomotive. So I took as my example the Clickspring youtube video where oil quenching tool steel is machined and hardened. I don't currently have any O1/O2 steel in bar form, but do have some 3/8" diameter O1 drill rod, so that was my material today.
The first order of business was to mill the rod flat to half its diameter. A shallower flat cut was also made to help alignment in the lathe tool holder.

Next, a 10-degree angle bar positioned the piece for cutting the relief angle.

Then the form for the 3/16" astragal was milled using the same size endmill. For a more complicated shape I'd use the CNC mill. I could also have drilled a 3/16" hole before milling the relief angle.

I heated it to bright red with a Mapp gas torch and quenched in lubricating oil. The result was a blackened surface, but seemed pretty hard when I attempted to file it. Then I tempered it with the torch, all rather a guessing game at the correct color, but the result was such that I could sharpen the edges with grinding wheel (oilstone would be more precise).
Testing on a piece of 3/4" brass went well. No chatter to speak of and a decent finish.

Came in to the house to find a free shipping offer from MSC, so ordered some oil hardening bar and some larger O1 drill rod.
I'll be away from home for the next two weeks as I visit Antarctica. Probably no models to visit there, but there is a steam train excursion that runs from Ushuaia and back.